Product and components
- Tablet and capsule counting
- Missing-product detection
- Component presence and orientation
- Colour, shape and surface checks
- Leaflet and insert presence
- Closure and tamper-evidence checks
Coordinate component checks, printed data, serialised codes, dynamic weight control and secure rejection around one validated production-line process.
A pharmaceutical inspection station must make the right decision and provide evidence that the intended product was checked and any failure was controlled. We engineer imaging, product handling, recipes, audit records, reject security and machine interfaces as one system.
The appropriate method is selected after the acceptance criteria, line speed, presentation and required evidence have been defined.
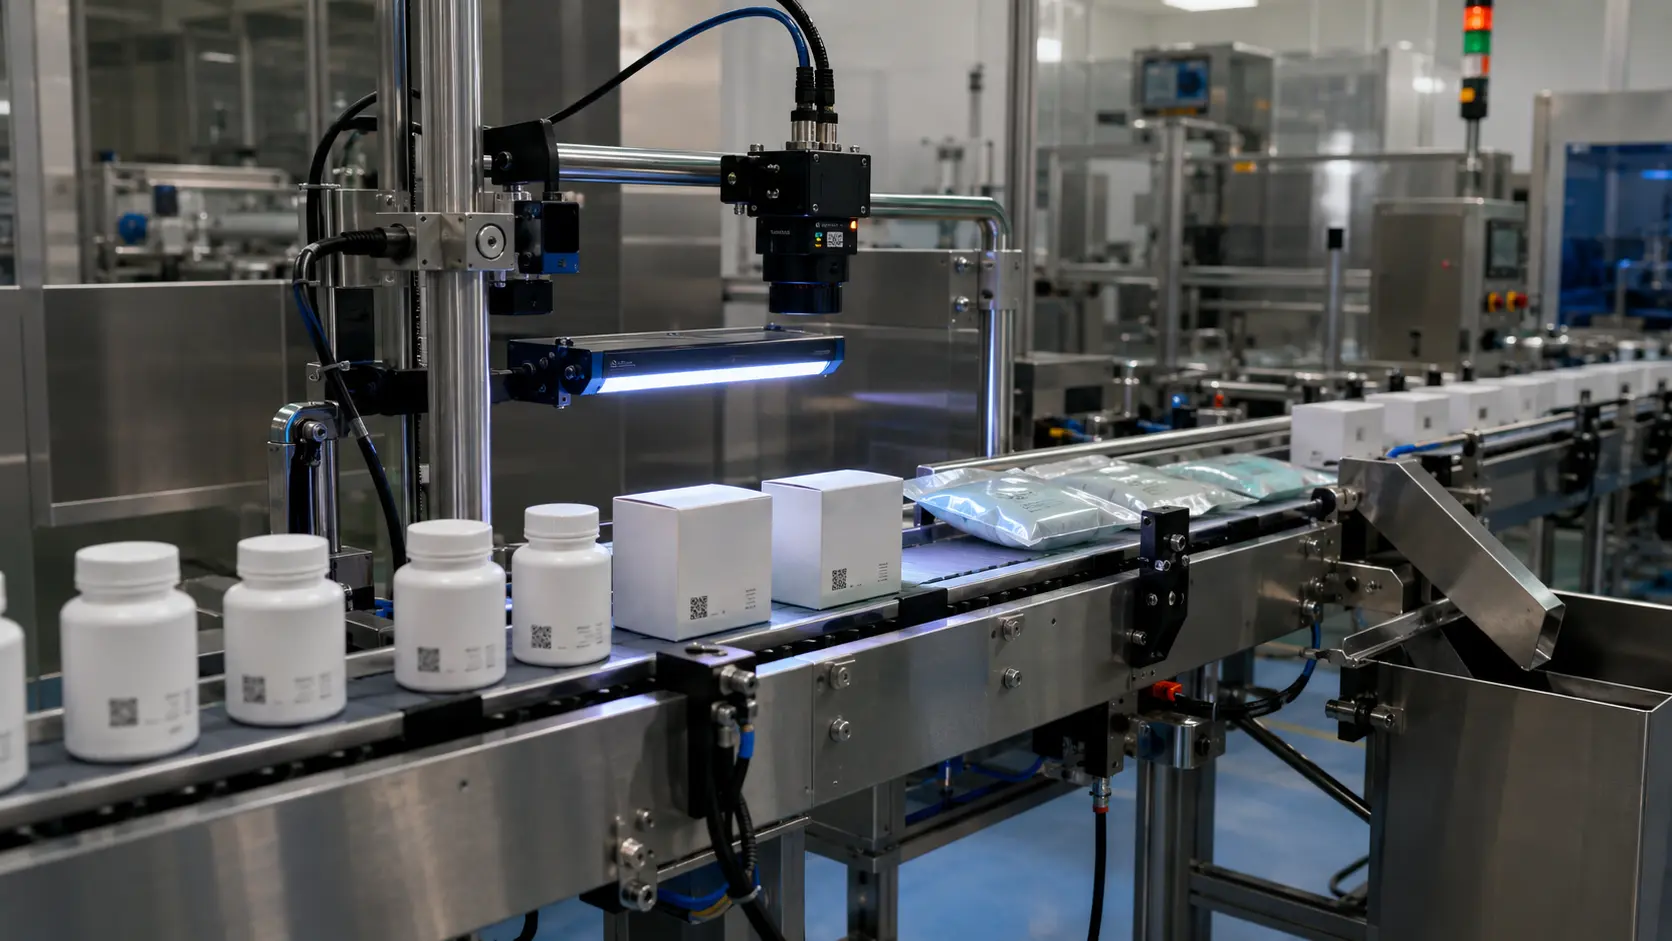
Rules-based vision is effective for stable geometry, presence, position, dimensions and print.
AI vision can help classify variable surfaces or natural appearance where fixed rules are too brittle.
Checkweighing can detect missing contents when the weight difference remains larger than normal process variation.
Code readers and OCR/OCV verify identity and variable data against the current job or database.
We define acceptance criteria, challenge sets, user access, recipe handling, data retention, alarms and reject tests before final sign-off.
Map each requirement to inspection, control, record or mechanical design.
Prove the critical checks with representative pass, fail and borderline samples.
Document recipes, faults, access, reject challenges and interfaces.
Complete production trials, training and agreed acceptance evidence.
We can review your URS, line data and samples before recommending hardware.
Ask an application question →Typical checks include component presence and orientation, print and artwork, OCR and OCV, Data Matrix and serial numbers, label identity, tamper-evident features and pack completeness.
It can when the missing component creates a stable, measurable difference relative to process and environmental variation. Representative trials establish the realistic detection window.
Projects can include reject confirmation, lockable reject bins, bin-full sensors, guarded access, air-pressure monitoring and fail-safe line-stop logic according to the agreed risk assessment.
Send the line format, required checks, representative samples, speed and validation expectations.