Products
- Liquid fill-level inspection
- Powder fill-level inspection
- Tablet and capsule counting
- Missing-product detection
- Overfill and underfill detection
- Component presence in kits
Detect missing product, overfill and underfill using the inspection method that matches your product, container and required evidence.
Clear liquids in transparent containers can often be measured with vision or optical sensors. Opaque containers, foaming products, powders and count-based fills may need different camera views, weight, X-ray or a combined approach. We select the method after testing the real product and pack.
Each check is configured against agreed samples, tolerances and fault responses. Multiple checks can be combined into a single inspection recipe.
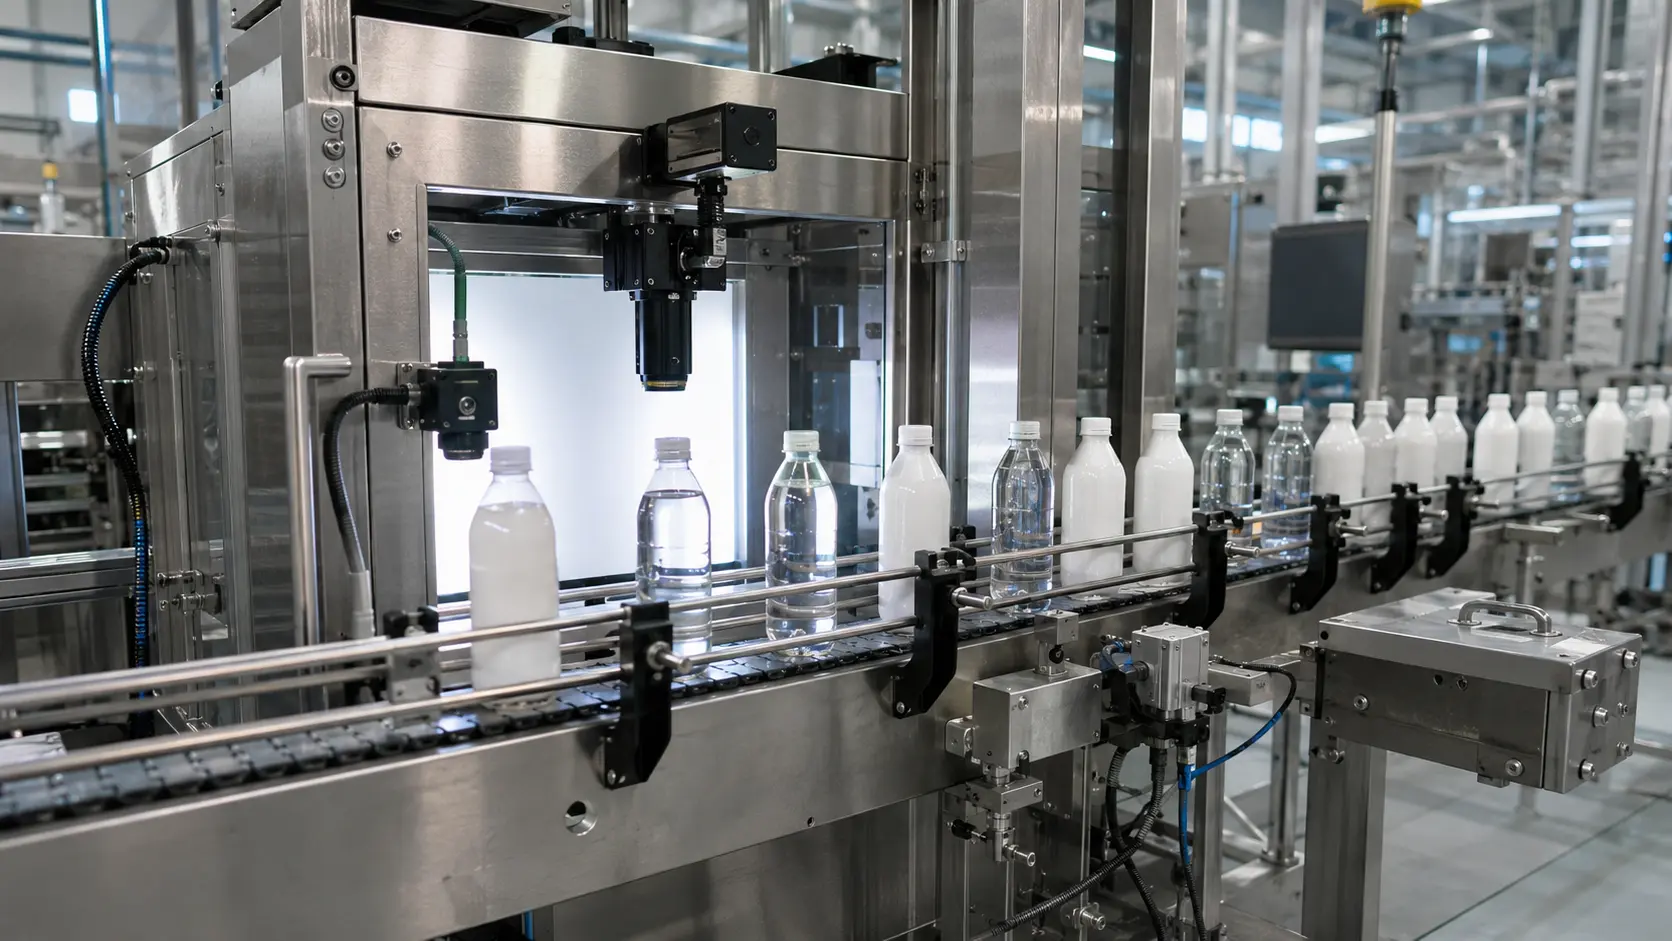
Assess product opacity, foam, meniscus, container colour and wall geometry
Separate normal fill variation from unacceptable fill conditions using production samples
Stabilise moving liquids when the required measurement demands it
Use complementary sensing where a single visual view cannot confirm the content
Provide trend outputs and controlled filler feedback where the upstream equipment supports it
Coordinate content inspection with cap, label, code and reject checks in one station where useful
We reduce risk early by proving the inspection on representative products before final hardware, handling and controls are committed.
Agree the pack, defect, speed, reject risk, data needs and acceptance criteria.
Run feasibility tests using representative good, bad and borderline samples.
Design handling, cameras, lighting, controls, guarding and rejection as one station.
Build, validate, install, train and support the system in production.
Need an answer for your exact product or line? Send us the application details and we will identify the next useful test.
Ask an application questionSometimes. Feasibility depends on the bottle transmission, product contrast, wall features and fill tolerance. Backlighting, near-infrared or another sensing method may help, but samples are essential.
Options include X-ray, checkweighing, capacitive sensing or an upstream view before closure. We choose the method according to product physics, pack format, accuracy and compliance needs.
Vision can count visible products before capping or inspect defined presentations. For closed opaque containers, weight or X-ray may be more appropriate.
Yes. Trend monitoring can identify drift and send warnings or controlled feedback to compatible filling equipment before the reject rate rises.
Send product details, target output, examples of acceptable and failed packs, and a short line video. We will define the most useful next technical step.