Flexible and tray packs
- Heat-seal inspection
- Tray-seal inspection
- Pouch-seal inspection
- Missing lidding film
- Folded or wrinkled seals
- Seal-width and continuity checks
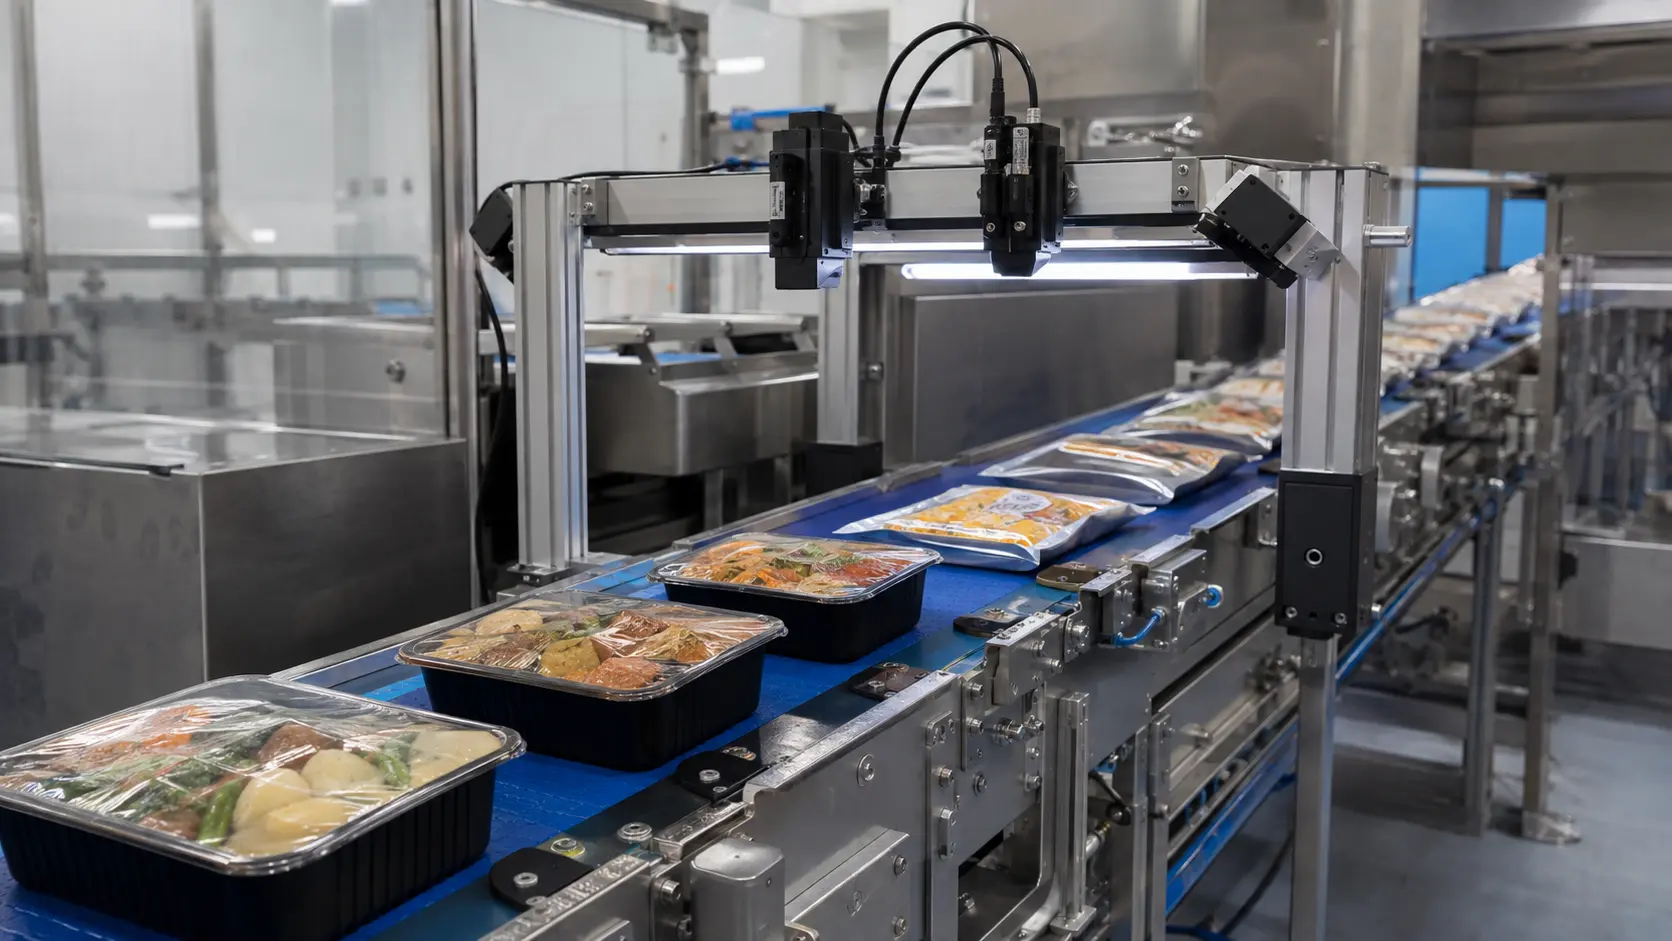
Detect visible seal contamination, folds, wrinkles, missing lidding film and closure faults with inspection engineered around the material and seal geometry.
Seal inspection is optically demanding: films are reflective, products vary, and contamination can resemble print or texture. We select camera angles, illumination and analysis methods from real samples, then integrate the outcome with rejection and line monitoring.
Each check is configured against agreed samples, tolerances and fault responses. Multiple checks can be combined into a single inspection recipe.
Define which visible conditions correlate reliably with unacceptable seals
Use representative products, films, print variants and contamination samples during trials
Avoid claiming detection of hidden seal strength where no visible evidence exists
Control film glare and transparent-layer reflections with the optical arrangement
Coordinate inspection timing with sealing machine indexes and pack spacing
Reject failed packs into a monitored bin or controlled lane appropriate to the risk
We reduce risk early by proving the inspection on representative products before final hardware, handling and controls are committed.
Agree the pack, defect, speed, reject risk, data needs and acceptance criteria.
Run feasibility tests using representative good, bad and borderline samples.
Design handling, cameras, lighting, controls, guarding and rejection as one station.
Build, validate, install, train and support the system in production.
Need an answer for your exact product or line? Send us the application details and we will identify the next useful test.
Ask an application questionVision can inspect visible features and defects, but it does not directly measure hidden bond strength unless a validated visual characteristic correlates with it. Destructive or specialist integrity testing may still be required.
Often it can detect visible product in the seal area. Detection depends on contrast, film print, contamination size, product variation and whether the area is optically accessible.
Yes, with suitable lighting and references, though clear reflective films require careful sample trials. The system can check presence, position and certain visible defects.
Options depend on the container and closure. Vision may detect visible evidence; other sensors can be integrated where the foil is hidden and a different physical principle is needed.
Send product details, target output, examples of acceptable and failed packs, and a short line video. We will define the most useful next technical step.